In optical and optoelectronic systems, unwanted reflections often degrade performance more than light leakage itself.
Applications such as camera modules, sensor systems, display assemblies, optical housings, and precision electronic modules frequently require materials that not only block light, but also suppress surface reflections that cause glare, ghosting, or optical noise.
Black & Matte PI Film (PNB) is engineered specifically for these environments, providing a uniform black, matte surface that effectively reduces reflection while maintaining high electrical insulation and dielectric strength.
With outstanding stability under extreme temperatures and strong dimensional reliability, PNB is widely used across electronics, aerospace, automotive, labeling, and insulation markets.
Engineers working on optical and light-sensitive systems often encounter:
Stray Light & Internal Reflection Unwanted reflections from internal components can introduce optical noise, affecting image quality and signal accuracy across optical and sensing systems.
Light Leakage & Optical Cross-Talk In compact and integrated designs, uncontrolled light propagation between components can degrade system performance and measurement reliability.
Increasing System Complexity & Miniaturization As systems become smaller and more integrated, managing light within confined spaces becomes more challenging.
Material & Integration Limitations Conventional solutions such as coatings may not be applicable to all surfaces, while some materials introduce risks such as particle contamination, outgassing, or assembly constraints.
In many cases, the problem is not insufficient light blocking, but uncontrolled reflection at material surfaces.
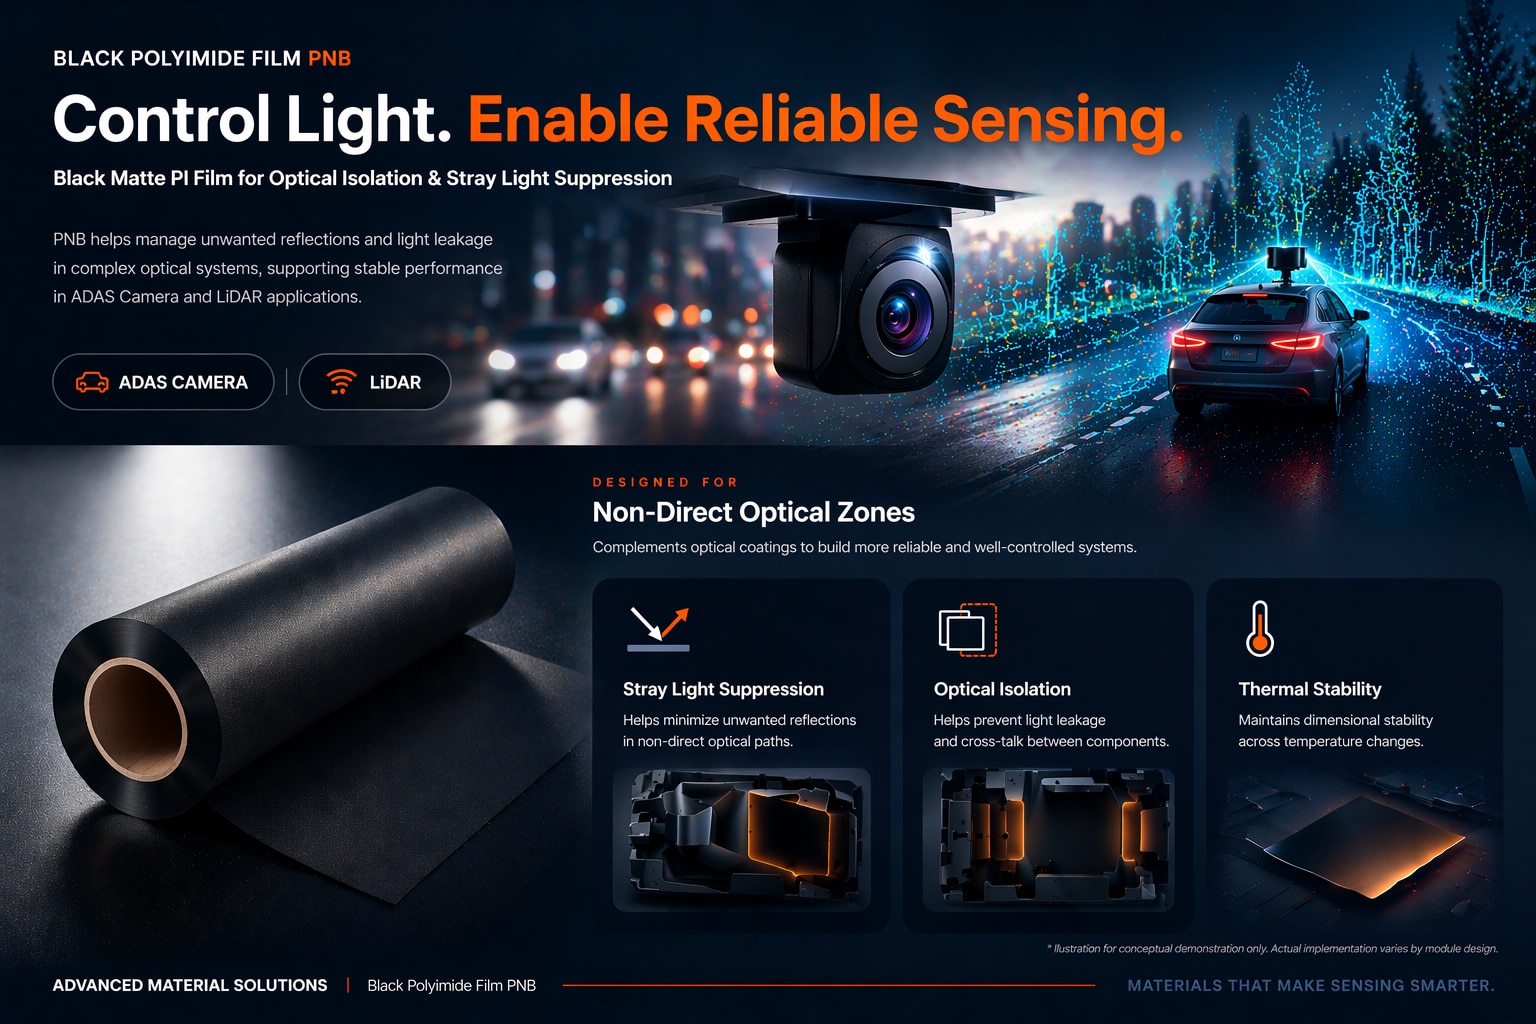
Our Black & Matte polyimide film PNB is engineered as a low reflection PI film, addressing stray reflections, reduce light leakage, and enable stable performance at the material and surface level, featuring:
Stray Light Suppression
Minimizes unwanted reflections from internal surfaces and components, improving signal clarity.
Optical Isolation
Helps prevent light leakage and cross-talk between adjacent elements in compact system designs.
Flexible System Integration
Thin, lightweight, and precisely processable for seamless integration into various module architectures.
Stable & Clean Performance
Designed for low particle generation and reliable operation under thermal and environmental stress.
Unlike glossy black or coated films, PNB is designed to deliver predictable, non-reflective behavior without compromising insulation reliability.
PNB is designed to integrate seamlessly into optical systems by complementing existing light control solutions. Rather than replacing optical coatings, it provides additional light management in areas where coatings are not applicable.
Around Sensitive Regions Used near sensing elements to reduce stray reflections and improve signal stability.
Between Internal Components Acts as an optical barrier to minimize light leakage and cross-talk within compact module designs.
Across Non-Direct Optical Zones Provides consistent light control in areas where coatings or surface treatments are not feasible.
By controlling reflection at the material surface, PNB helps engineers improve optical signal quality without adding mechanical complexity.
Precision Light Control for LCD Backlight Modules
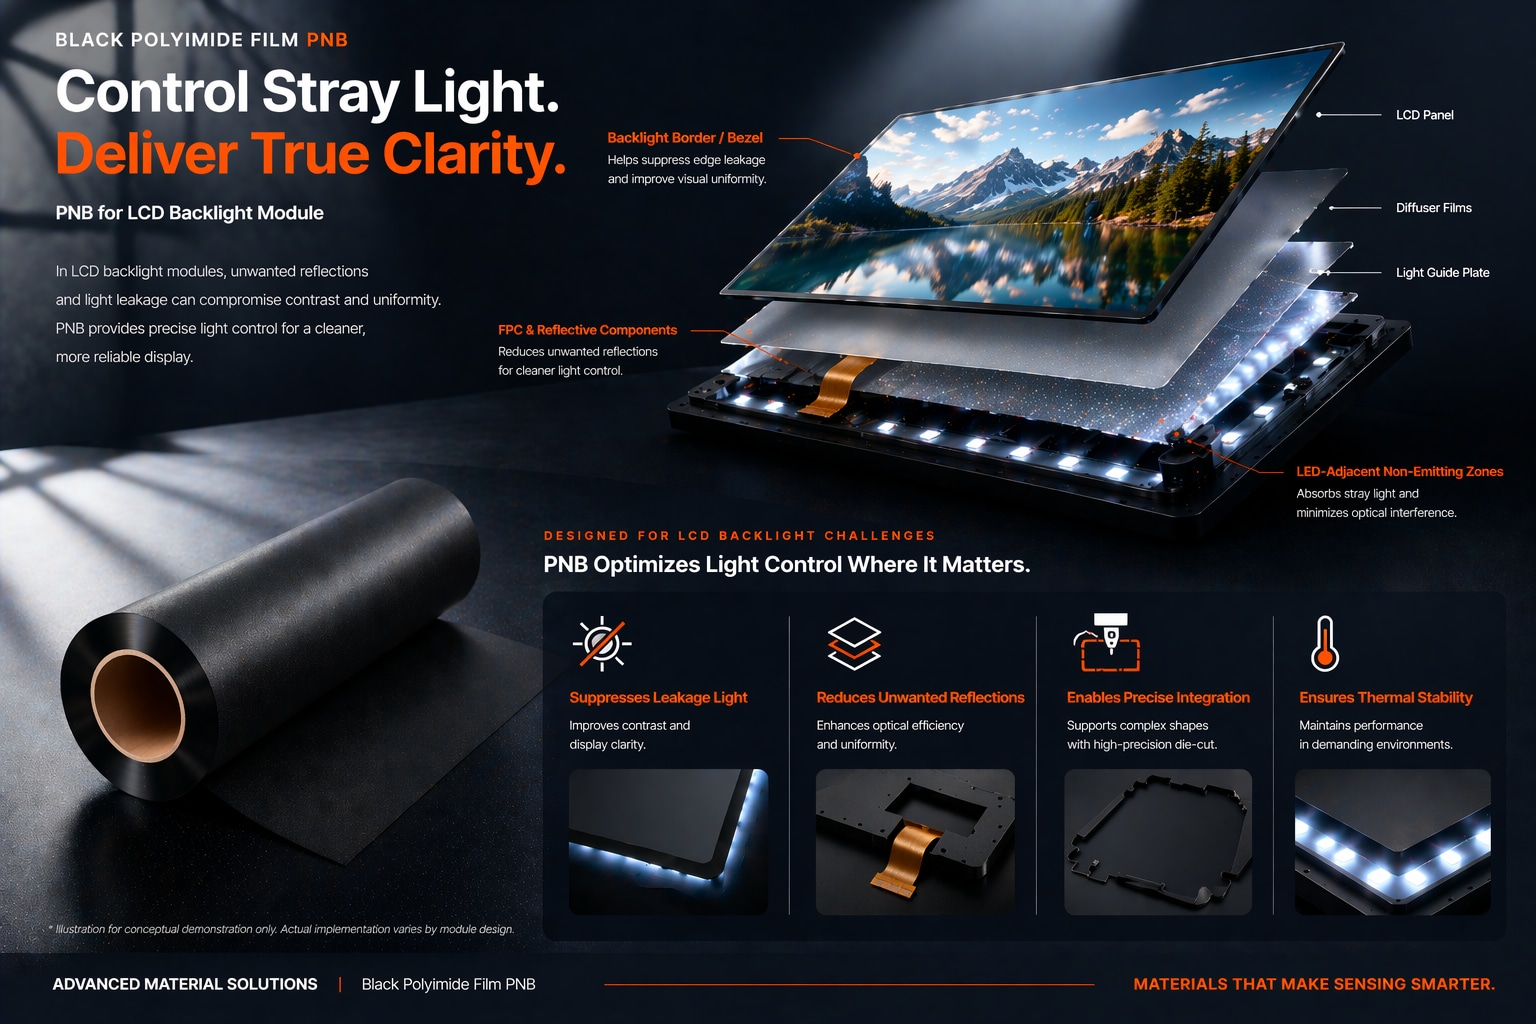
PNB is a black matte polyimide film engineered for light shielding and optical isolation in LCD backlight modules. It effectively suppresses leakage light and unwanted reflections in non-emitting areas, helping improve contrast, uniformity, and overall display clarity without affecting primary light output.

Contact us to discuss Black & Matte Polyimide Film (PNB) solutions optimized for your reflection sensitivity, insulation requirements, and integration constraints.
Taiwantrade.com and iDealEZ.com uses analytical cookies and other tracking technologies to offer you the best possible user experience. By using our website, you acknowledge and agree to our cookie policy.
For more information on cookies or changing your cookies settings, read Taiwantrade & iDealEZ’s Privacy Policy.
